Snack Categories Used in Private Label Programs
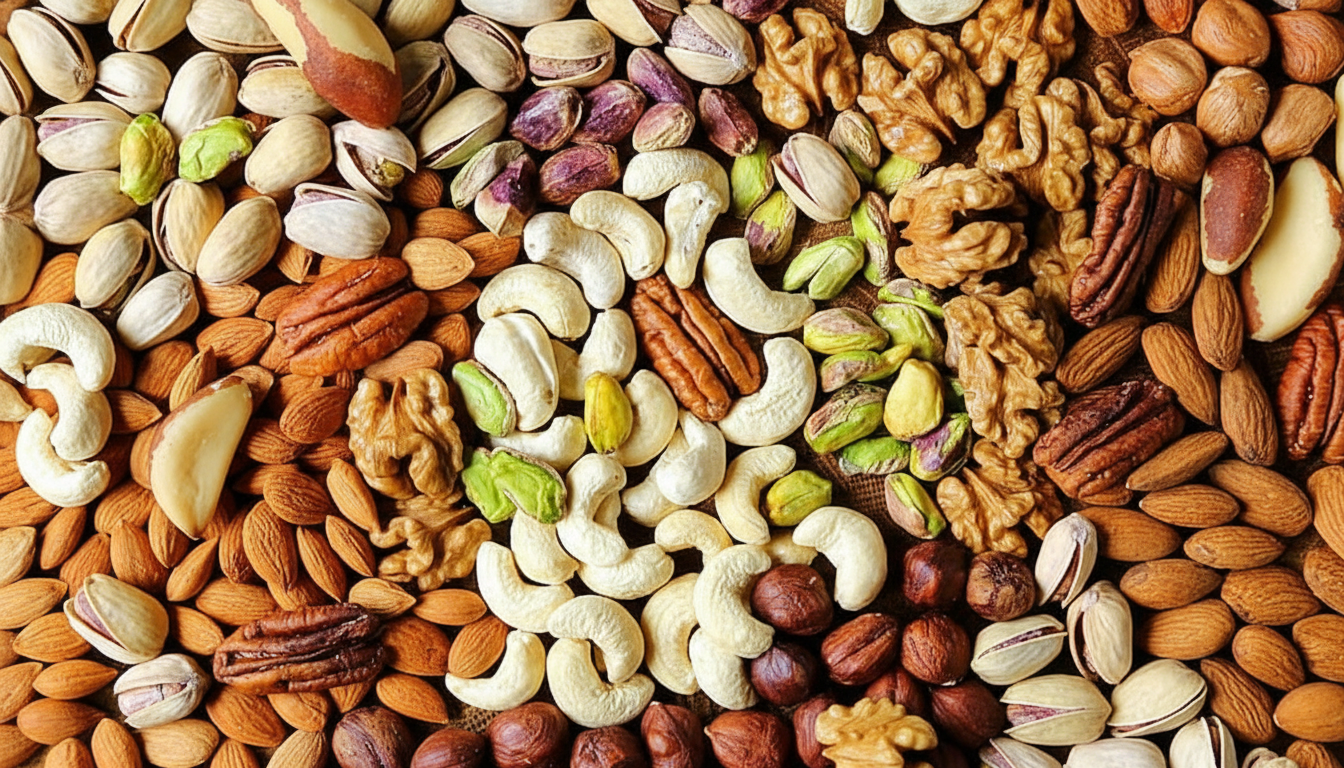
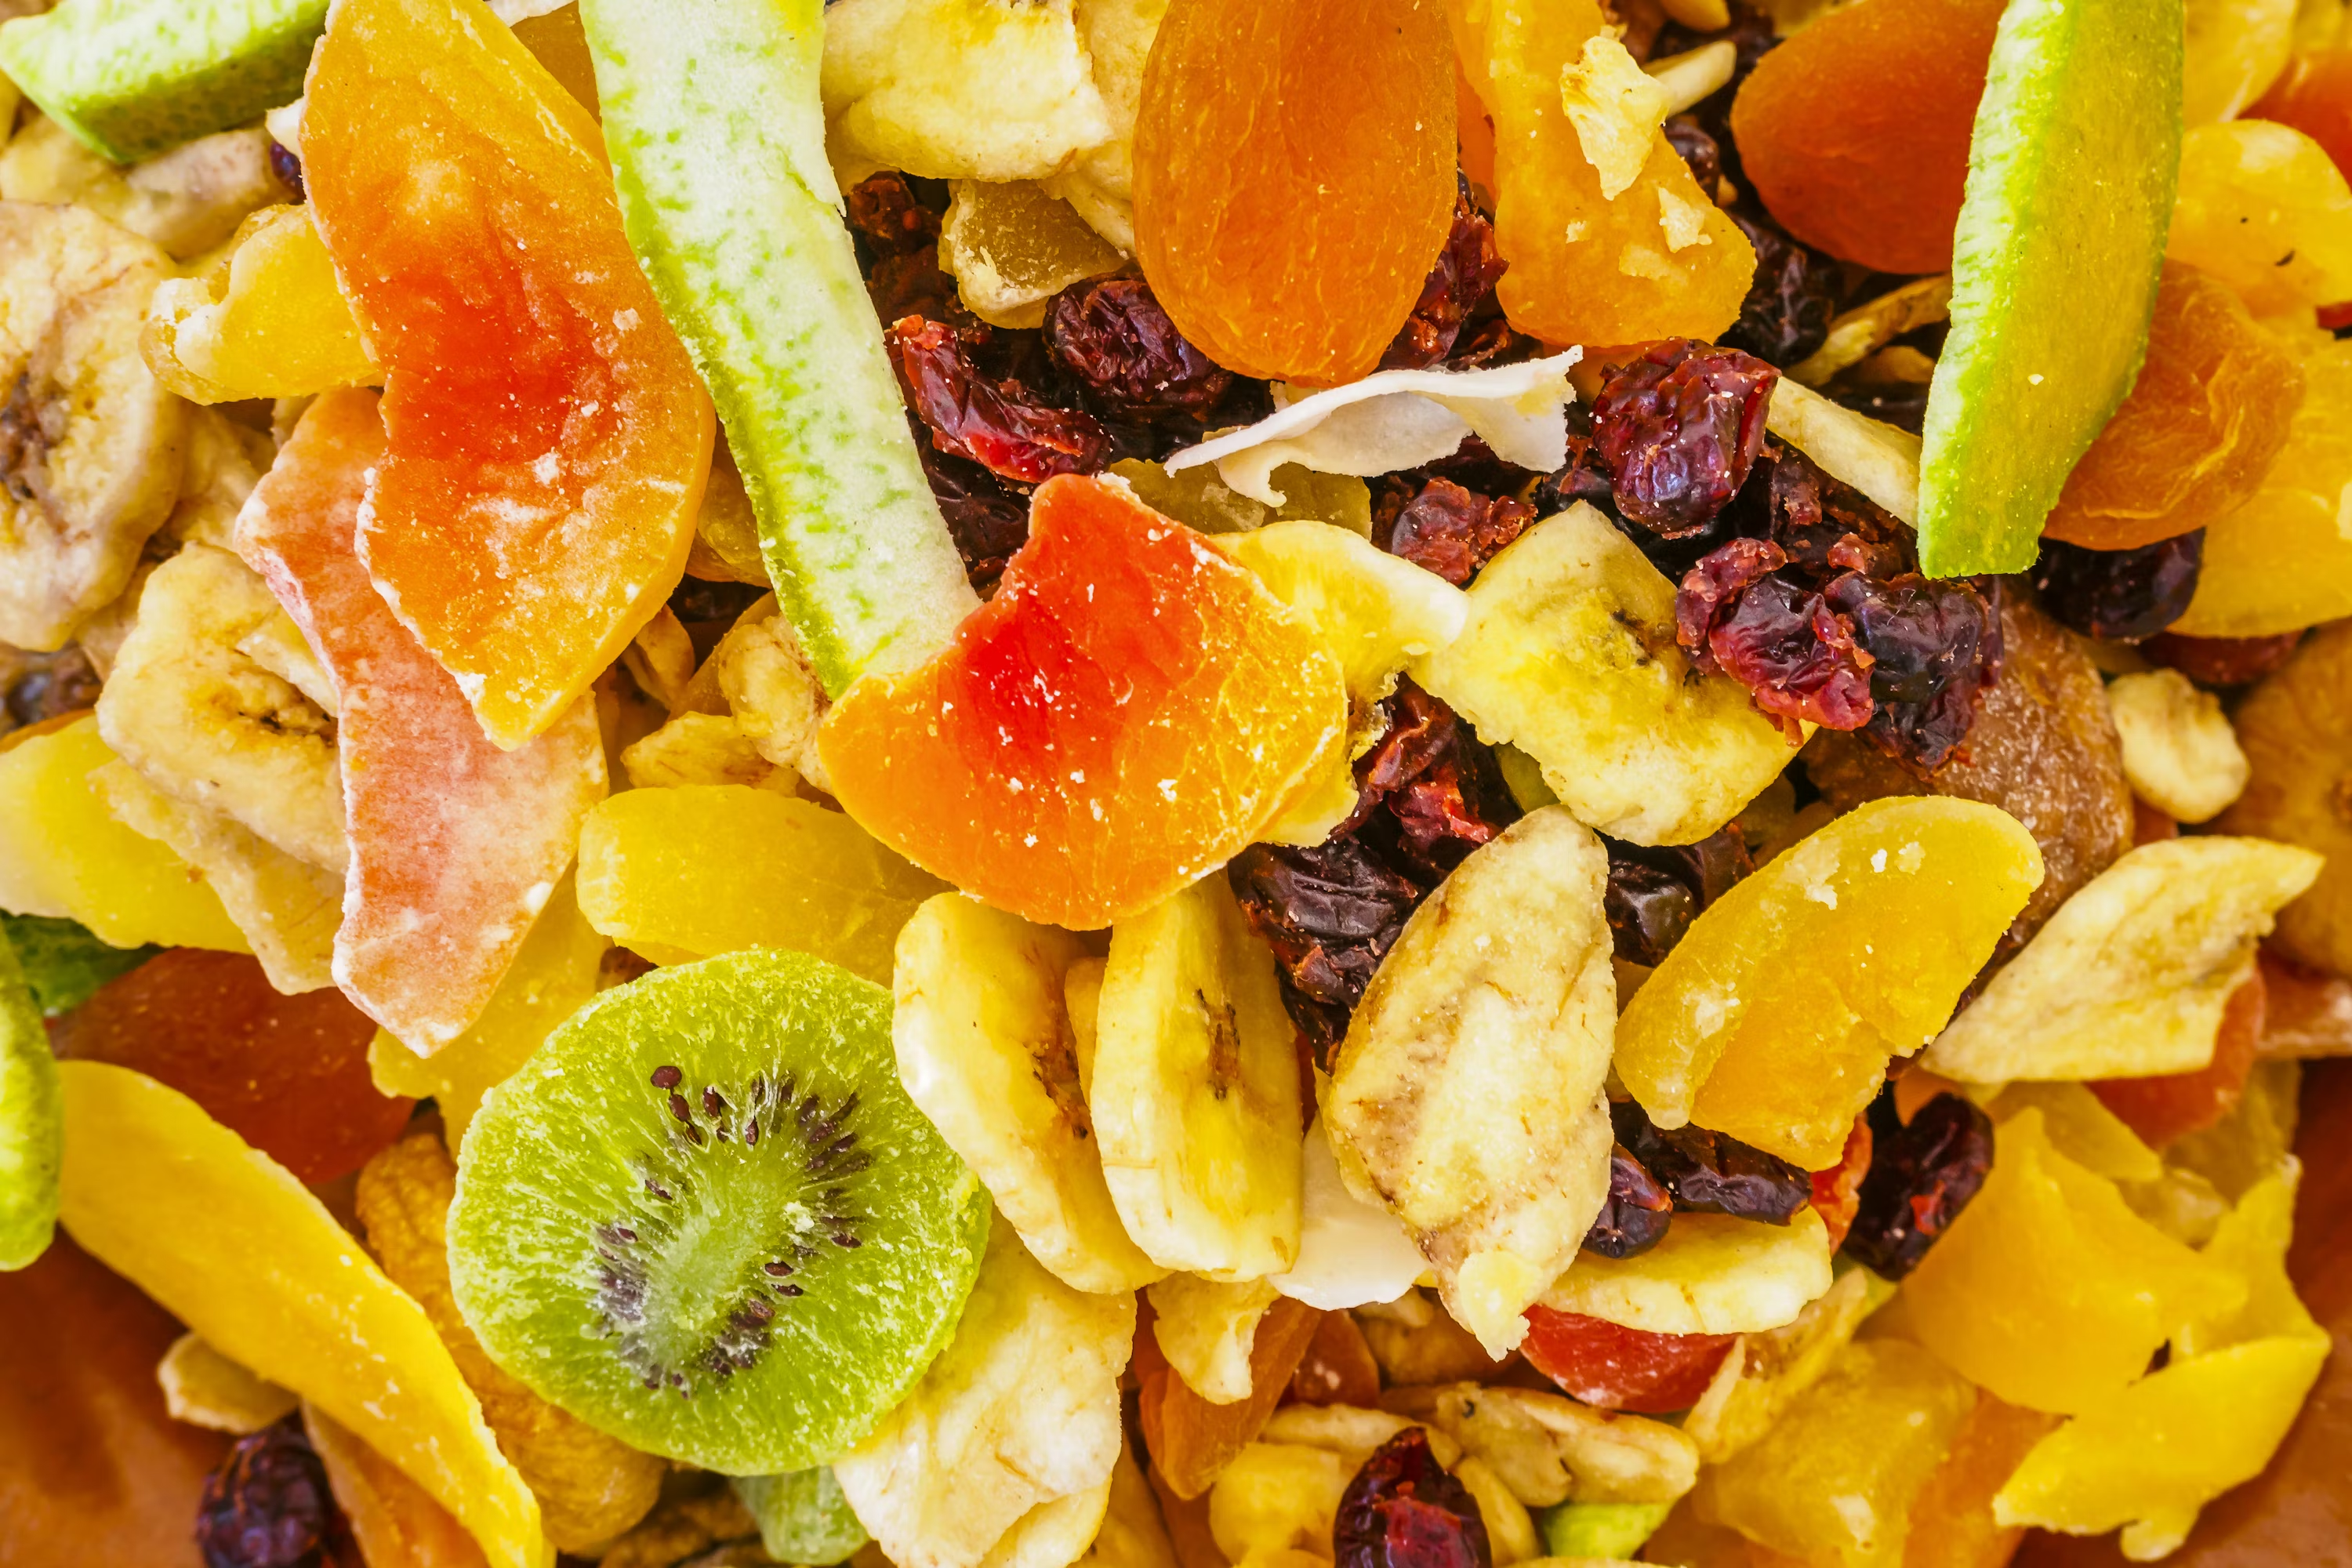
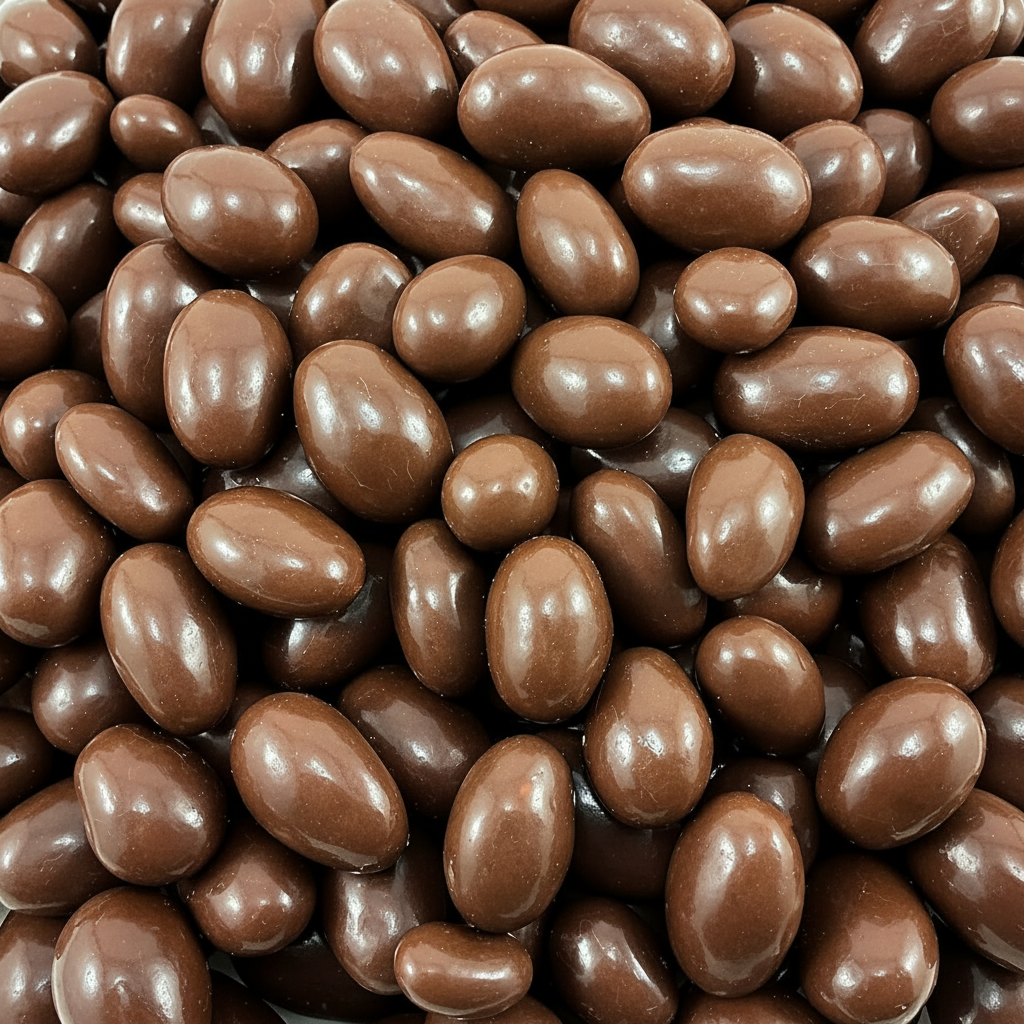
Private label snack programs span a wide range of product categories. Each category has different production requirements, packaging considerations, and retail positioning strategies.
An overview of how private label snack products are developed, manufactured, and packaged for retail distribution.
Start a Private Label Snack ProgramPrivate label snack manufacturing is the process of producing snack food products that are sold under a retailer's or brand owner's own label rather than the manufacturer's brand. The manufacturer — often called a co-packer or contract manufacturer — handles the production side while the brand owner controls marketing, distribution, and pricing.
This model has become the foundation of modern grocery retail. Major supermarket chains, convenience store brands, specialty food retailers, and online sellers all use private label manufacturing to offer differentiated products with better margin control than they get from national CPG brands.
In the snack category, private label manufacturing covers roasted and flavored nuts, trail mixes, dried fruit blends, chocolate-covered snacks, candy assortments, snack mixes, and seasonal specialty items. The manufacturer sources raw materials, manages recipe development, runs production, performs quality assurance, and delivers finished goods in retail-ready packaging.
At L'Orenta, we operate as an SQF-certified private label snack manufacturer producing products across every major snack category from our facility in San Antonio. We manage the full production cycle from raw ingredient intake through palletized shipment to distribution centers.
Retailers and brand owners choose private label manufacturing for strategic and financial reasons that go beyond simple cost savings.
Build a proprietary snack assortment that strengthens your retail identity and gives customers a reason to choose your store over competitors.
Create unique flavor profiles, packaging designs, and product formats that national brands cannot match in your specific market.
Private label products typically deliver 10 to 15 points of additional gross margin compared to equivalent national brand products in the same category.
Customers who buy your private label products can only get them at your stores, creating repeat visits and long-term loyalty to your brand.
Private label snack programs span a wide range of product categories. Each category has different production requirements, packaging considerations, and retail positioning strategies.
The right packaging format drives shelf presence, product protection, and consumer convenience. L'Orenta's automated packaging lines support every major retail snack format.
Flat bottom gusset for shelf stability, resealable zipper, large front panel for branding. Available from grab-and-go single-serve to family-size formats.
Enhanced structural rigidity with premium gravure printing. Popular for specialty retail and club store environments.
Individual portion-controlled packets bundled into overwrapped or boxed multi-packs. Ideal for schools, offices, and variety packs.
Large-format heavy-gauge film packaging designed for warehouse club retailers with specific pallet pattern requirements.
From initial product concept through retail distribution, the manufacturing process follows a structured workflow managed by your co-packing partner.
Define your product vision, target category, flavor profiles, weight specifications, and packaging preferences.
Source raw materials from qualified suppliers with full traceability and quality documentation.
Precise recipe execution using automated blending systems for consistent flavor and texture.
Multi-head weighing, filling, sealing, metal detection, and lot coding on high-speed lines.
Weight verification, seal integrity, visual inspection, and microbial testing before release.
Palletized shipment to distribution centers with full lot documentation and compliance records.
See our facility tour or private label process for a detailed walkthrough of each step.
Food safety is non-negotiable in private label snack manufacturing. Major retailers require GFSI-benchmarked certification as a minimum threshold for vendor consideration. At L'Orenta, our food safety standards meet the requirements of the most demanding retail programs.
GFSI-benchmarked food safety and quality certification covering our entire production process from receiving through shipment.
Documented hazard analysis and critical control point programs that identify and control food safety risks at every production stage.
Multi-head weighing accuracy, inline metal detection, seal integrity verification, and lot-level documentation on every production run.
Lot tracking from raw ingredient receipt through finished product shipment, supporting 4-hour mock recall requirements for retail compliance.
Private label snack programs serve every major retail channel. Each channel has specific packaging, compliance, and distribution requirements.
National and regional grocery retailers building store-brand snack assortments with competitive pricing and premium quality.
Learn MoreSingle-serve and grab-and-go snack formats designed for impulse purchase and high-traffic retail environments.
Learn MoreLarge-format bulk packaging with specific pallet configurations and member-value positioning for warehouse club channels.
Learn MoreBulk and private label products for foodservice distributors supplying restaurants, hotels, and institutional accounts.
Learn MoreDirect-to-consumer snack brands requiring shelf-stable packaging optimized for individual parcel shipping and unboxing experience.
Learn MoreSelecting the right snack co-packer is one of the most consequential decisions a brand owner makes. The manufacturer you choose affects product quality, food safety compliance, speed to market, and long-term scalability. Here are the factors serious buyers evaluate:
Does the manufacturer have automated equipment, sufficient capacity for your volume, and experience with your product category? Visit the facility and see the lines in operation.
Verify GFSI-benchmarked certification (SQF or BRC), HACCP compliance, and FDA registration. Ask for audit scores, not just certificates. Major retailers will audit your manufacturer.
Confirm the manufacturer supports your required packaging — stand-up pouches, doypacks, multi-packs, club store formats. Ask about minimum print runs and packaging development support.
Evaluate palletizing capability, freight relationships, EDI compatibility, and experience shipping to major distribution centers. Geographic location impacts total delivered cost.
Your first order might be one pallet. Your tenth order might be a hundred. Choose a manufacturer whose capacity can grow with your program without requiring you to switch partners.
L'Orenta serves as a manufacturing partner for brands at every stage. Whether you are launching your first product or managing an established multi-SKU program, our nationwide co-packing capability and SQF-certified facility are built to support your production needs.
Full-service private label snack production.
Learn MoreContract snack packaging and co-packing services.
Learn MoreRetail-ready contract packaging for snack brands.
Learn MoreIndustry guides and manufacturing resources.
Learn MoreWork with an SQF-certified snack manufacturer built for retail. From formulation through palletized shipping, we handle every step of the production process.
Typically responding within 24 hours · For qualified high-volume projects · Built for retail-ready production
Start a Private Label Snack Program© 2026 L'Orenta Nuts — San Antonio, Texas. SQF Certified Snack Manufacturer.