SQF Certified · HACCP Verified · GMP Compliant · FDA Approved
Step Inside
Our Facility
From hygiene-controlled entry to final pallet loading, see exactly how your product moves through our operation.
Walking Into the Facility
Located in San Antonio, Texas, our free-standing, fully climate-controlled facility was purpose-built for snack manufacturing at scale — designed from the ground up for safety, precision, and consistent production year-round.
Controlled Entry and Hygiene Protocol
Every L'Orenta team member follows documented hygiene and gowning procedures before entering production zones. Access is controlled to protect product integrity and food safety.
- Hand washing and sanitizing stations
- Smocks, hairnets, beard nets, gloves
- Allergen zone awareness
- Visitor protocols
- GMP Certified
Precision Automated Production
Product is portioned using calibrated multi-head weighers and packed on automated doypack lines designed for consistent throughput and repeatable results.
In-Line Quality Verification
Every package passes through metal detection and check-weigh systems. Critical control points are monitored and recorded under our HACCP plan. An automated reject system removes any bag that does not meet quality standards.
Step 05
Take a closer look.
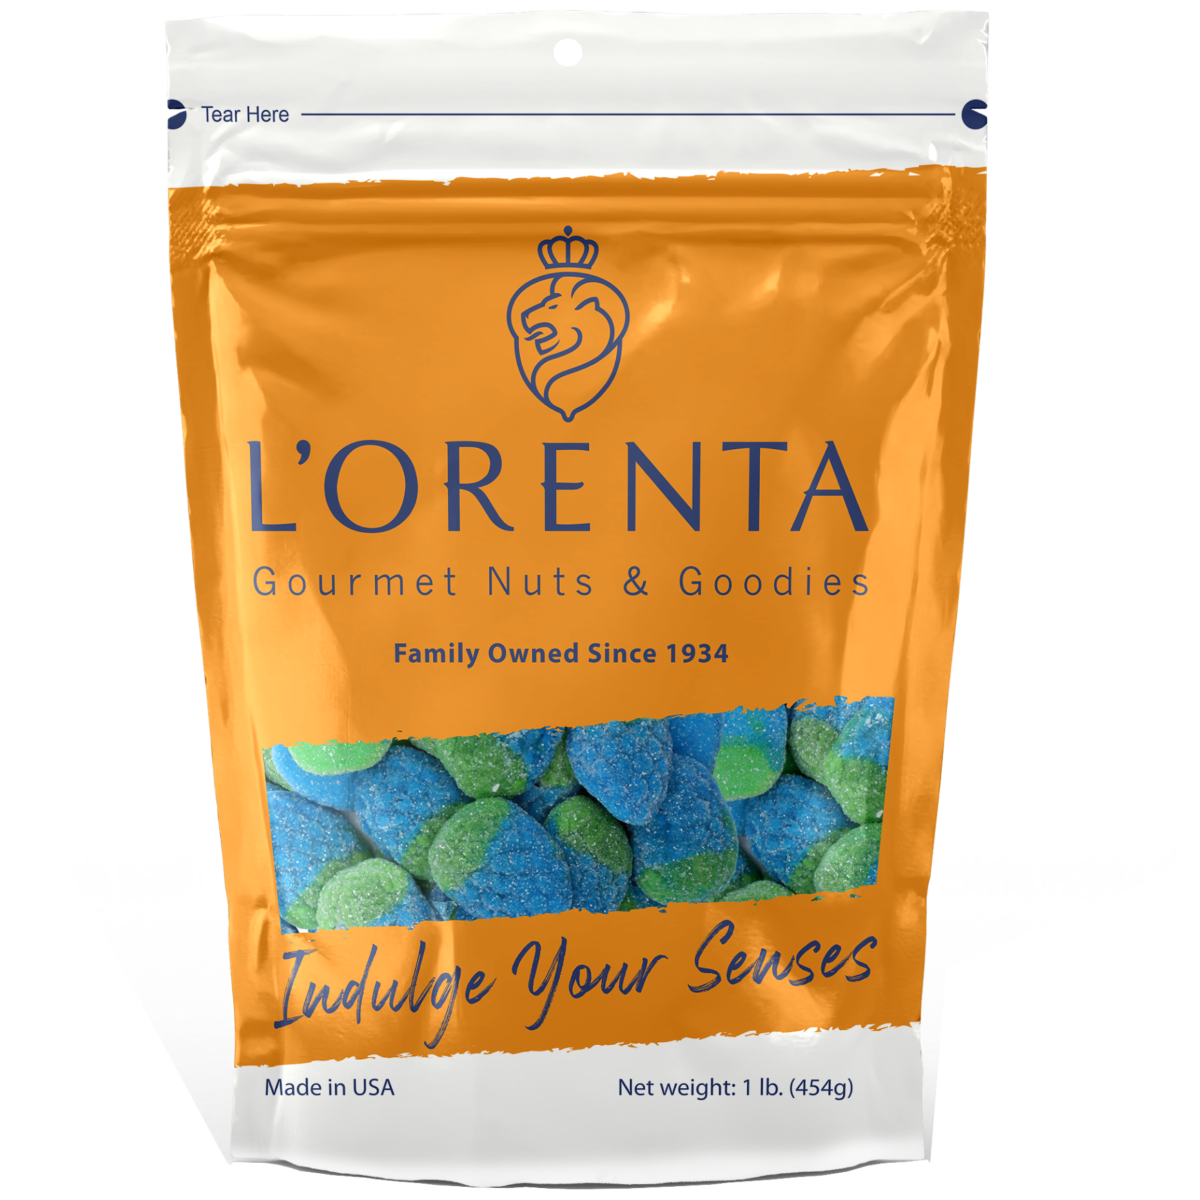
Every bag is quality inspected to ensure seals, zippers, and overall packaging meet our standards before packing.
Many other styles available. Bags can be produced with or without hang holes, resealable zippers, tear notches, windows, and more. The features shown above are just examples.
Hang Hole. Die-cut hang hole centered above the seal line for pegboard-ready retail display. Reinforced to support full bag weight.
Resealable Zipper. Press-to-close zipper to easily reseal bags.
Tear Notches. Precision-cut tear notches on both sides with a dashed guide line for easy, controlled opening.
Custom Branding Zone. Full-bleed print area for your private label artwork. Logo, brand name, and product identity — all customizable.
Product Window. Clear window lets customers see the real product before purchase, reinforcing freshness and quality. Custom window shapes available to match brand identity.
Net Weight. Accurate fill weight verified by inline check-weigh systems.
Product Credentials. Clear, credible product claims that help customers shop with confidence. Many different styles and designs — bags can include or omit hang holes, resealable zippers, windows, and more.
Retail-Ready Packaging and Labeling
Finished pouches are labeled, coded, and packed into retail-ready cases. Private label branding and UPC integration are handled in-house.
- Custom private label packaging
- Date and lot coding
- Barcode and UPC integration
- Club and display-ready formats
Palletization, Staging, and Distribution
Cases are palletized, wrapped, and staged under FIFO inventory control. Verified pallets are then scheduled and loaded for regional and national distribution.
Next Step
Ready to Scale
With Confidence?
Partner with a facility built for precision, speed, and retail success.
Explore Our Manufacturing Services
From private label copacking to wholesale distribution, our SQF-certified facility supports retail snack programs at every scale.
Private Label Snack Manufacturing
Build your own branded snack line with our automated production and custom packaging.
Learn MoreSnack Co-Packing Services
Full-service co-packing from ingredient sourcing to retail-ready packaging.
Learn MoreWholesale Snacks
Browse wholesale nuts, trail mix, dried fruit, and candy for retail resale.
Learn MoreNationwide Coverage
Snack manufacturing and distribution serving all 50 states.
Learn MoreKnowledge Center
Expert guides on manufacturing, food safety, and wholesale distribution.
Learn MoreFood Safety Standards
SQF, HACCP, GMP certifications that back every product we manufacture.
Learn MoreThe same SQF-certified facility produces every program we ship — our wholesale nuts, wholesale candy, wholesale trail mix, and wholesale dried fruit orders, plus custom private label nuts, private label trail mix, private label candy, and full private label snack manufacturer runs.
© 2026 L'Orenta Nuts — San Antonio, Texas. SQF Certified Snack Manufacturer.